Air blast
Fast and compact for suitable lightweight, stable packs when the required trajectory and compressed-air supply are available.
A weight result only protects production when the correct item is removed and its removal is confirmed. We select the reject principle around pack behaviour, throughput, available length and the way your quality team needs to contain and reconcile non-conforming product.
A reject system is dependable only when the failed product remains tracked, is removed or contained as intended, and produces the defined response after an uncertain reject.
Fast and compact for suitable lightweight, stable packs when the required trajectory and compressed-air supply are available.
A positive mechanical action for cartons, tubs, bottles and other packs that can tolerate controlled side contact.
Useful for small, difficult or fast-moving packs where a downward reject path provides dependable separation.
Appropriate where automatic removal is unsuitable, space is restricted, or the process requires operator intervention before restart.
The fastest or heaviest product is not always the hardest to reject. Light empty packs, unstable tall containers, sticky pouches and closely pitched cartons can be more demanding. Trials should cover the complete product range, including start-up, back-to-back packs and fault recovery.
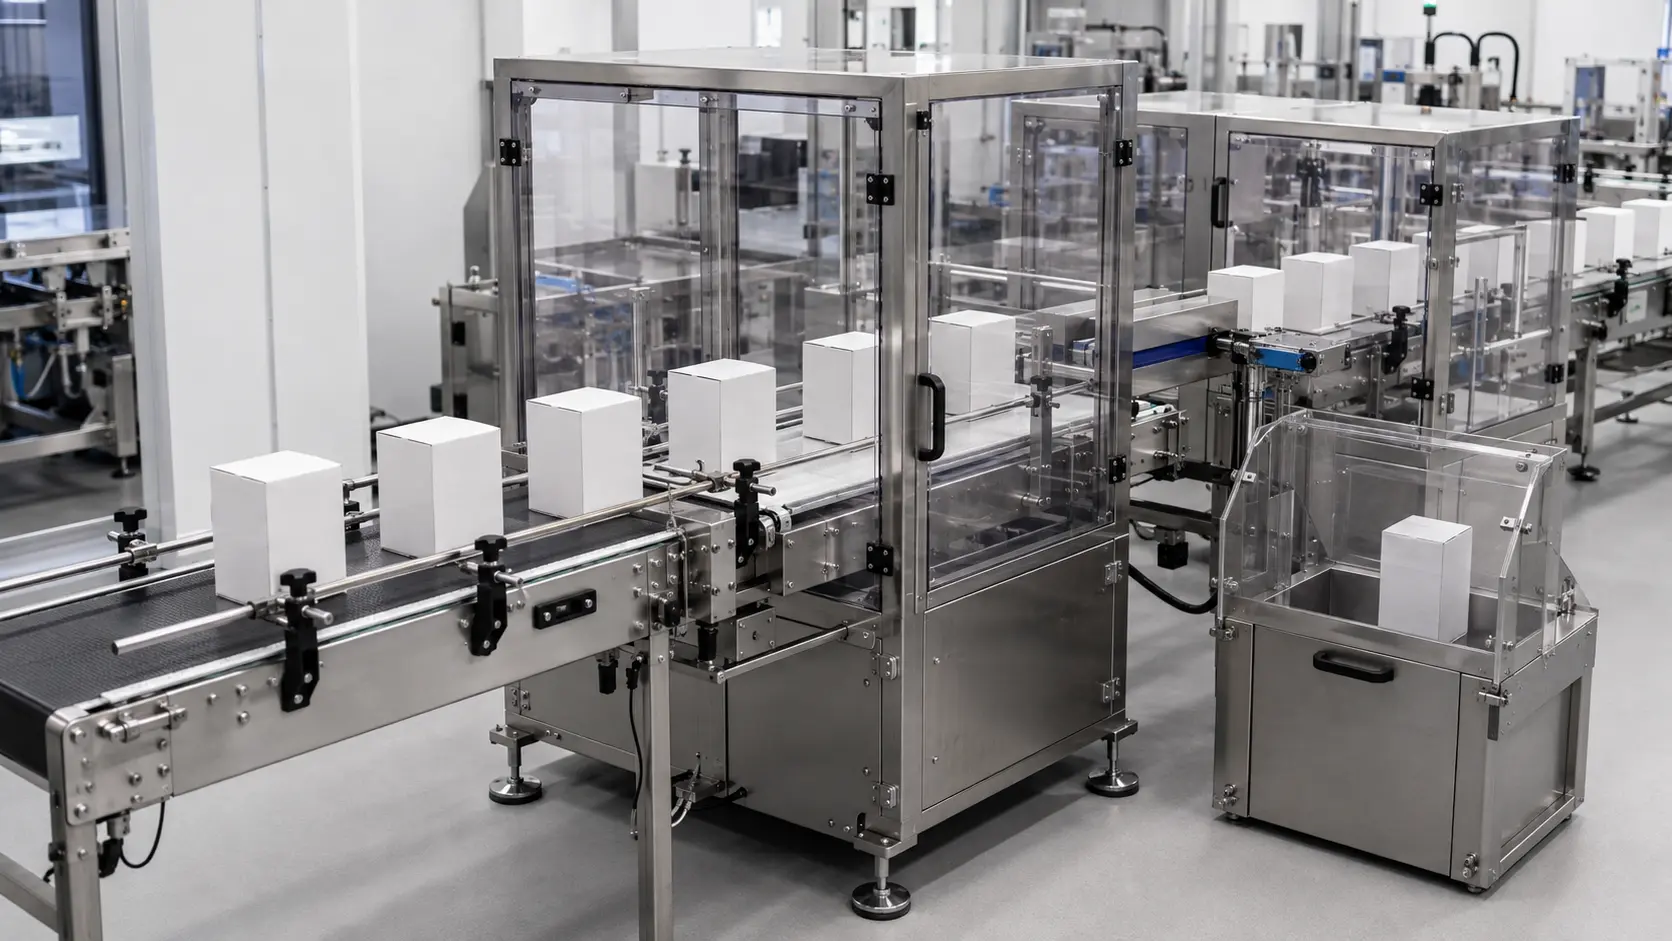
A shared reject route can handle weight, metal, barcode or vision faults only when each result remains associated with the correct product and reconciliation procedure.
Discuss integrated inspectionThese answers help match reject mechanism, confirmation, containment and failure response to the actual pack and production risk.
There is no universal best type. Pack weight, stability, speed, pitch, available space and containment needs determine the safest reliable method.
The control tracks the classified product to the reject point and expects a sensor response in a defined window. A missing response can raise an alarm or stop the line.
Yes, where separate reject devices or a suitable diverting arrangement are justified by your procedure and footprint.
Yes. Lockable containment and monitored access can be included for higher-control applications.
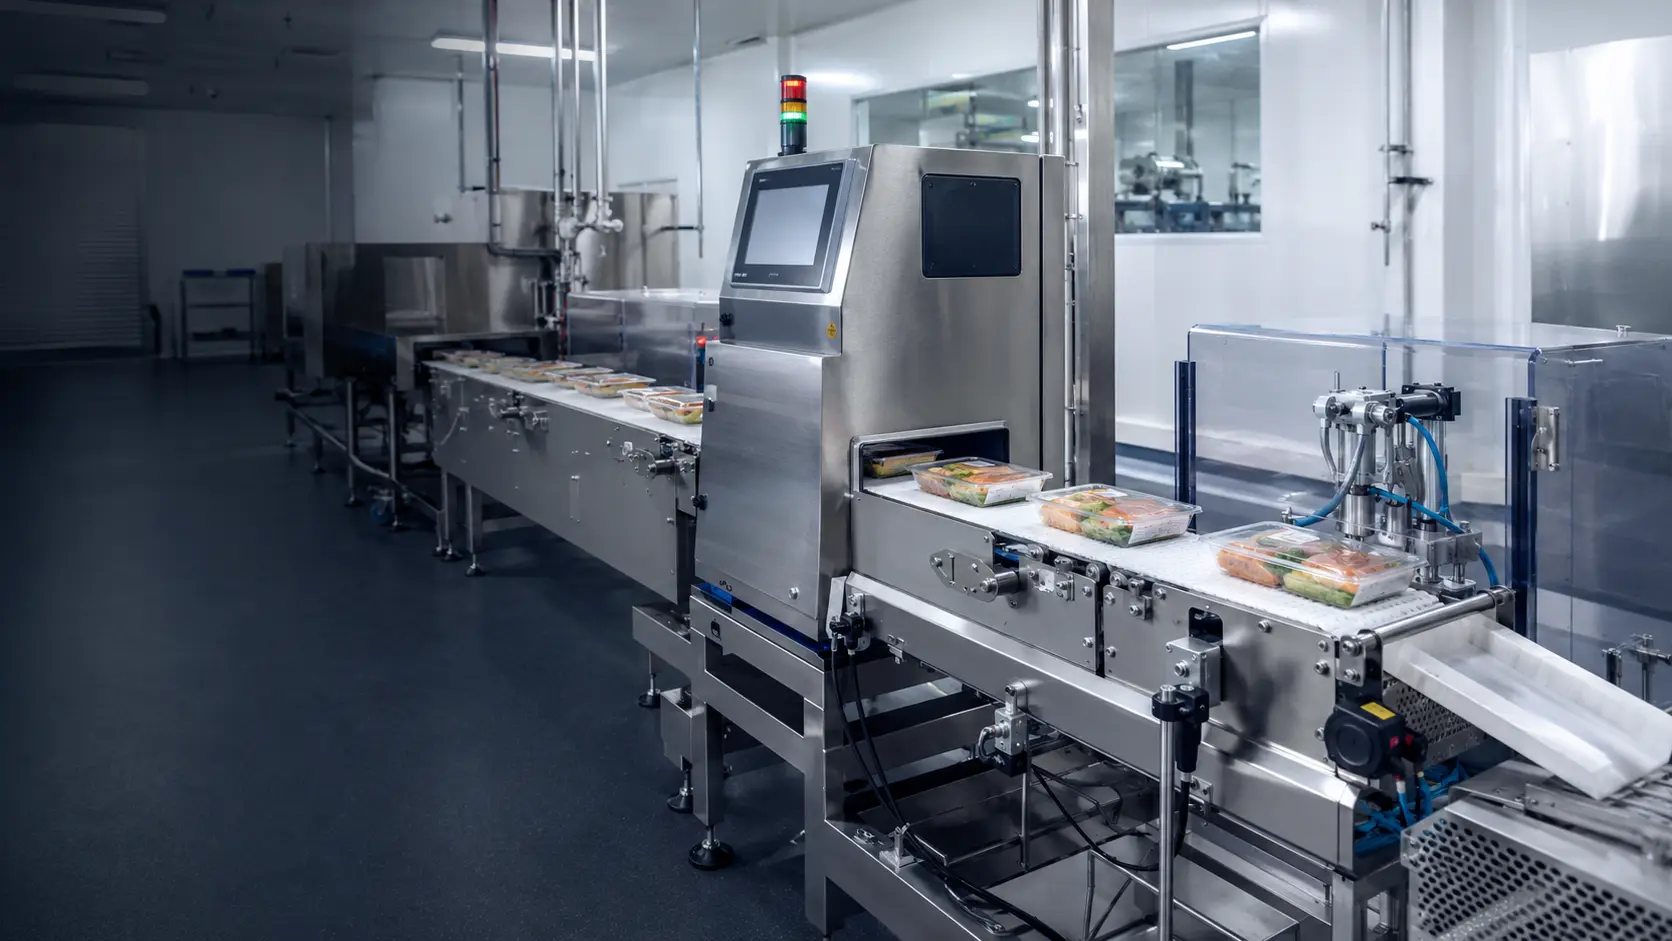
Inspect correctly presented packs at the agreed production rate, classify them against defined limits and remove non-conforming items with an application-matched reject system. We configure the weighing conveyor, controls, reject method and data outputs as one practical system.
Explore system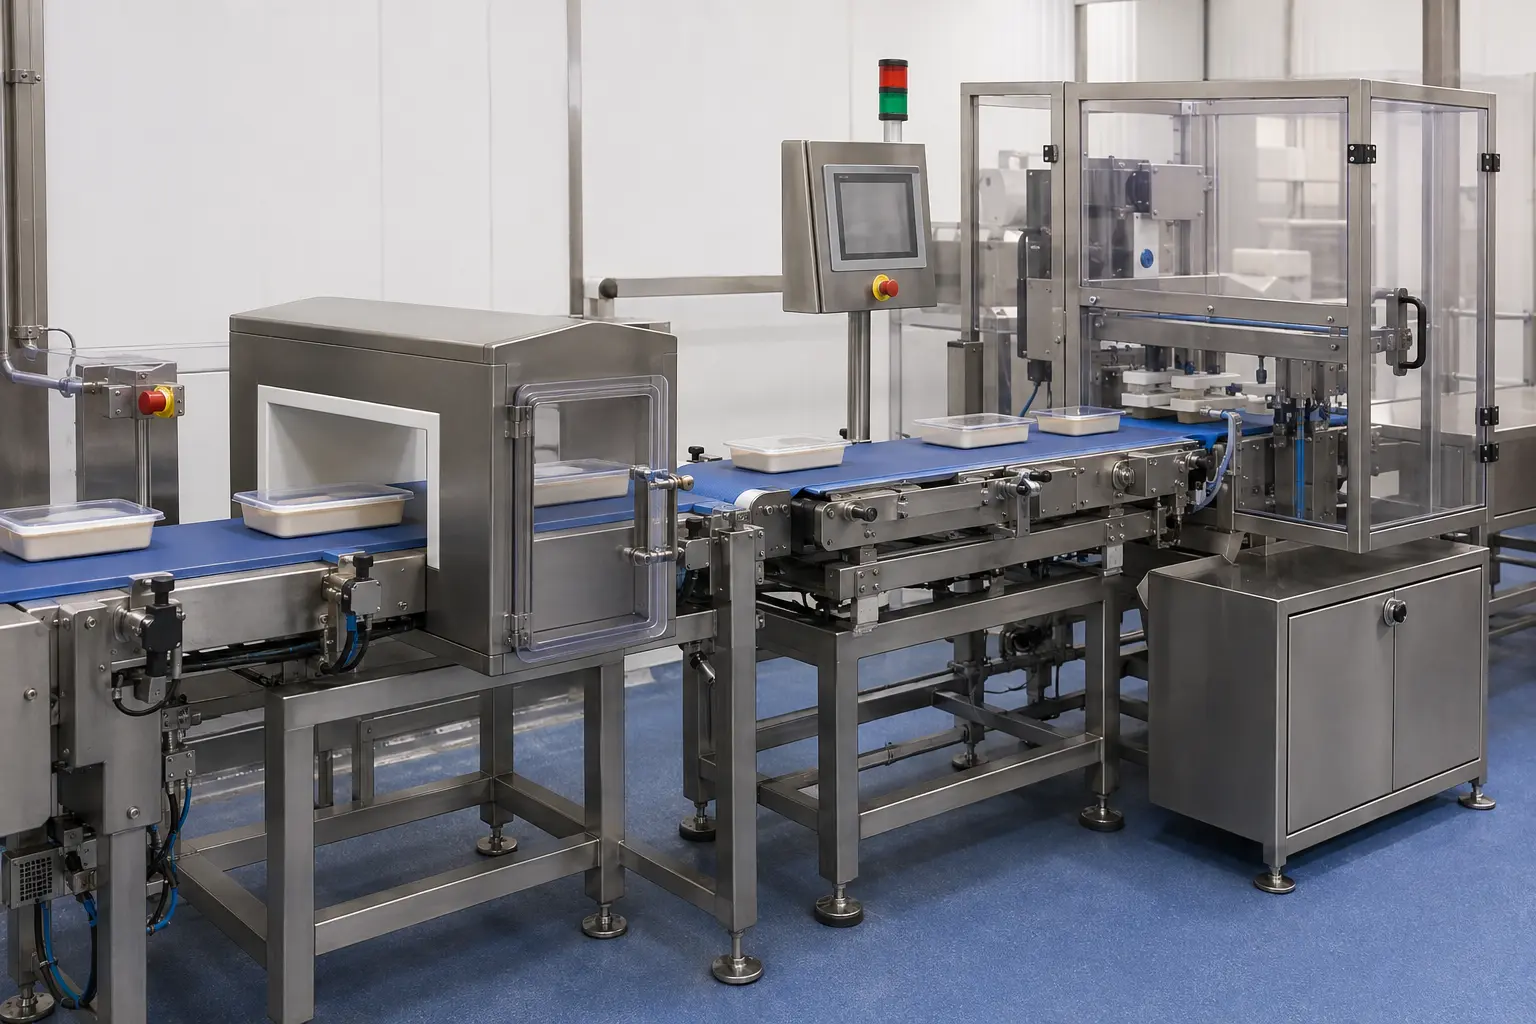
Bring contaminant detection and automatic weight inspection together in a coordinated system. A combination unit can reduce footprint, simplify product transfer and provide a consistent reject and line-control philosophy while keeping the two inspection results distinct.
Explore system
Make weight inspection information useful beyond the machine HMI. From simple batch reports to line-level data exchange, we define the records, identifiers, retention and interfaces your production and quality teams actually need.
Explore systemUse the next guide that matches the engineering or quality question behind your project.
Share pack details, target weights, line speed and any inspection or data requirements.